


Get In Touch With Us
Connect with Metals-Tech
Ready to take the first step towards unlocking opportunity realizing goals, and embracing innovation?
-
 CALL ANY TIME
-
 Follow Us
LinkedIn
-
 Say Hello
info@metals-tech.com
In the precision cold rolling of aluminium strips, heating up the side areas of the work roll barrels is critical to prevent the “tight edge” phenomenon—a localized increase in strip edge thickness and hardness caused by excessive heat loss at the roll ends. This defect leads to poor flatness, edge cracking, and significant yield loss in high-value products.
Metals-Tech’s Electromagnetic Work Roll Heating System with our partners provides an advanced, targeted solution to this persistent challenge. Unlike hot edge spray method, our system utilizes precisely controlled electromagnetic induction to apply direct, localized heat to the work roll barrels, with a focus on maintaining optimal thermal crown—especially at the critical roll edges.By integrating this innovative system, aluminium producers can dramatically reduce edge-related scrap, expand the operational window for challenging alloys and gauges, and achieve a new level of thickness consistency and strip shape—directly translating to higher yield, reduced finishing costs, and entry into more demanding market segments.

Related Solutions





Related News
From Capacity to Manufacturing Value Metals-Tech Enables High-End Stainless Steel and Superalloy Plate Production
31 August 2026
Full-line automation and process intelligence for high-performance materials in demanding industries In today’s stainless steel industry, capacity is no longer the most important question. Large-scale production lines, impressive annual output figures and broad product catalogues are no longer enough to define competitiveness. As the market becomes more price-sensitive and conventional stainless steel products face increasing pressure, the real value of a modern plate production line lies in a different question: Can it manufacture difficult materials, in flexible batches, with stable quality and fast delivery? This question is especially important for high-end stainless steel and special alloy plate products, including duplex stainless steel, super duplex stainless steel, super austenitic stainless steel, nickel-based corrosion-resistant alloys, high-temperature alloys and precipitation-hardening stainless steels. These materials are not ordinary commodities. They are used in chemical equipment, energy systems, marine engineering, pressure vessels, heat-resistant components, high-end manufacturing equipment and critical industrial applications. Customers do not only buy steel plate. They buy reliability, delivery certainty, process confidence and long-term material performance. Metals-Tech provides full-line Electrics, Automation and Digital solutions for advanced plate production lines, helping producers transform complex special alloy manufacturing into a stable, traceable and high-value industrial capability. The Market Is Changing: From Volume Production to Specialized Manufacturing China does not lack stainless steel capacity. It does not lack production scale. What the market increasingly needs is the ability to respond to complex orders. Special alloy plate orders are often very different from conventional mass-production orders. A chemical project may require 2205 duplex stainless steel, 2507 super duplex stainless steel and nickel-based alloy plates at the same time. The order volume may be limited, the specifications may be scattered, and the technical requirements may include special heat treatment, ultrasonic testing, surface inspection, tight dimensional tolerance and strict delivery schedules. For large-scale production systems, such orders are difficult to organize. Mills prefer continuous production: one grade, one process route, one large batch and long rolling campaigns. But special alloy customers often require the opposite: This is why the high-end plate market requires a new type of production capability: not only strong equipment, but also strong process organization, process control and digital quality management. High-End Stainless Steel and Superalloy Plate: Why It Is Difficult The term “high-end material” is often used too easily. In real manufacturing, these materials are difficult not because they sound premium, but because their process windows are narrow and their quality risks appear early. For conventional stainless steel, stable production is already important. For high-alloy materials, it becomes critical. The final plate quality is affected by many upstream and downstream factors: Process FactorInfluence on Final Plate QualityChemical composition controlDetermines corrosion resistance, strength and phase balanceInclusion and cleanliness controlAffects UT result, fatigue behavior and reliabilitySolidification conditionInfluences segregation, internal defects and hot workabilityReheating scheduleDetermines temperature uniformity and deformation readinessRolling pass scheduleAffects grain structure, plate shape and dimensional accuracyTemperature windowCritical for duplex steel, nickel alloys and high-temperature alloysHeat treatmentDetermines final microstructure and mechanical propertiesCooling controlInfluences phase transformation and property stabilitySurface treatment and picklingDetermines surface quality and downstream usabilityInspection and traceabilityProvides quality evidence for critical applications Materials such as 2507, alloy 625, C276 or 800H cannot be understood simply as steel with more nickel, chromium or molybdenum. Each grade has its own hot workability, precipitation sensitivity, solution annealing requirement, cooling requirement and quality risk. If the process window is missed, later finishing cannot fully recover the internal quality. Full-Process Manufacturing: The Real Foundation of Special Alloy Plate For high-performance plate production, each process section must be connected into one coherent system. Rolling, heat treatment, pickling, straightening, inspection and finishing cannot operate as isolated islands. A modern special alloy plate line needs integrated control across the complete route. This complete process chain is especially important for small-batch, multi-grade and high-specification orders. The producer must know not only whether a plate is qualified, but also how that quality was created. Four-High Reversing Plate Mill: Flexibility for Complex Materials For high-end stainless steel and special alloy plate, a four-high reversing plate mill provides important manufacturing flexibility. It allows the production of different grades, thicknesses and widths with controlled pass schedules and process adaptation. However, the rolling mill itself is only part of the answer. To produce difficult materials consistently, the automation system must coordinate rolling force, screwdown, roll gap, plate temperature, pass reduction, speed, descaling, plate tracking and operator guidance. Metals-Tech’s automation solutions support: Control AreaTechnical ValuePass schedule controlStable deformation path for different grades and thicknessesRolling force and gap controlImproved thickness accuracy and plate geometryTemperature trackingBetter control of hot-working windowSpeed and drive coordinationStable rolling process and reduced disturbancePlate trackingAccurate material identity throughout the lineOperator guidanceMore consistent execution of complex rolling proceduresData collectionFoundation for process analysis and quality improvement For high-temperature alloys and nickel-based alloys, rolling stability is not only a productivity issue. It is directly related to internal quality and final material performance. Heat Treatment: Where Material Performance Is Finalized Heat treatment is one of the most critical steps in high-end stainless steel and superalloy plate production. For many special alloys, rolling creates the geometry, but heat treatment defines the final performance. Duplex stainless steels require proper phase balance. Super austenitic stainless steels require corrosion resistance and structural stability. Nickel-based alloys require controlled solution treatment and stable microstructure. Precipitation-hardening stainless steels require precise heat treatment to achieve target strength and performance. Metals-Tech’s furnace automation and process control functions help manage: Heat Treatment ControlQuality ContributionFurnace temperature uniformityReduces property variation across plate length and widthHeating curve controlEnsures correct thermal history for each gradeSoaking time managementSupports uniform microstructureCooling process trackingImproves repeatability of final propertiesRecipe managementReduces manual error for multi-grade productionBatch and plate trackingLinks heat treatment data with final inspection result In high-end material production, heat treatment is not a secondary process. It is a core value-creation process. Inspection and Traceability: From Qualification to Customer Confidence For special alloy plate, qualification is not only about passing inspection. It is about proving the full manufacturing history. Customers in demanding industries often require ultrasonic testing, penetrant testing, dimensional inspection, surface inspection, mechanical testing, corrosion-related testing and full material certification. A modern production line must connect these results with process data. Metals-Tech’s digital quality management system enables coil- or plate-based process genealogy, including: Data CategoryTypical InformationMaterial identityHeat number, grade, specification and order routeRolling historyPass schedule, force, gap, speed and temperatureHeat treatment historyFurnace number, recipe, temperature curve and timeSurface treatmentPickling, finishing and surface quality dataInspection resultsUT, PT, dimensional inspection and final judgmentDelivery recordPlate identity, certificate data and customer requirement This digital quality passport is essential for high-value customers. It supports root-cause analysis, customer audits, process improvement and long-term product development. From “Can Produce” to “Can Produce Stably” In the special alloy industry, there is a major difference between producing one qualified batch and producing stable quality over many years. The first qualified heat proves capability.Repeated qualified production proves maturity. A producer may successfully manufacture a difficult grade once or twice. The real test begins when the same grade must be produced repeatedly under changing conditions: different customers, different thicknesses, different widths, different heat numbers, different delivery times and different technical requirements. At that stage, the process database becomes one of the most valuable assets of the enterprise. Metals-Tech helps producers build this asset by connecting automation systems with process data, quality data and production records. Over time, this creates a knowledge base for: Grade-specific rolling windows Heat treatment recipes Defect root-cause analysis Plate shape and thickness control optimization Yield improvement Delivery performance improvement Customer-specific technical requirements Continuous process learning This is how manufacturing experience becomes digital capability. The Value of Flexible Special Alloy Production High-end stainless steel and superalloy plate production is not only about making the most difficult grade. It is about responding to real customer needs. Many customers do not require the largest volume. They require the right plate, in the right specification, with the right certificate, at the right time. For chemical equipment manufacturers, energy projects, marine engineering companies or high-end machinery builders, the value of fast and reliable delivery can be greater than a small material price difference. A delayed plate may delay an entire project. This creates strong value for producers who can combine: CapabilityCustomer ValueMulti-grade productionOne-stop supply for complex projectsSmall-batch flexibilityBetter response to scattered demandFast deliveryReduced customer project delay riskProcess stabilityLower quality uncertaintyFull inspectionHigher confidence in critical applicationsTechnical supportFaster solution when specifications changeDigital traceabilityStronger evidence for audits and certification In high-end material markets, the customer is not simply buying tonnage. The customer is buying manufacturing reliability. Metals-Tech's Role in High-End Plate Automation Metals-Tech provides full-line automation and digital solutions for advanced plate production. Our capabilities cover Level 0 instrumentation, Level 1 basic automation, drive systems, Level 2 process models, HMI/SCADA, data systems, production tracking and quality management. Core solution areas Metals-Tech SolutionApplication ValueFull-line automationCoordinates rolling, heat treatment, pickling, straightening and inspectionPlate tracking systemEnsures material identity across the complete processRolling process controlImproves thickness, shape and rolling stabilityFurnace automationSupports precise heat treatment and recipe executionInspection data integrationLinks quality results with production historyDigital quality managementCreates traceable process and product recordsProcess optimizationSupports stable production of complex gradesLifecycle serviceHelps producers improve performance after commissioning Through these solutions, Metals-Tech helps customers move from equipment operation to process intelligence. High-End Materials Need High-End Control The future of stainless steel and special alloy plate will not be decided by capacity alone. It will be decided by the ability to manufacture difficult products consistently. For duplex stainless steel, super duplex stainless steel, super austenitic stainless steel, nickel-based corrosion-resistant alloys, high-temperature alloys and precipitation-hardening stainless steels, every process step matters. Melting quality, reheating, rolling, heat treatment, finishing, inspection and traceability must work together. This is the core direction of the modern special alloy plate industry. Conclusion: The Next Stage Is Not Bigger, but Deeper The stainless steel industry has already built enough capacity. The next stage of competition will not be defined only by who can produce more, but by who can produce better, faster and more reliably for demanding applications. High-end stainless steel and superalloy plate production requires a deeper form of capability: metallurgical understanding, flexible production organization, precise automation, robust heat treatment, reliable inspection and digital process traceability. Metals-Tech is committed to supporting this transformation. By providing full-line automation and full-process quality management solutions, Metals-Tech enables plate producers to build stable, repeatable and high-value manufacturing capability for the most demanding materials. In the future, the strongest producers may not be those who say, “We can make everything.”They will be those who can clearly define their strongest grades, their strongest specifications and the industries they serve best. For high-end stainless steel and superalloy plate, real competitiveness is not only measured in tons. It is measured in process depth, quality stability and the ability to solve difficult customer problems.
Read More
Building the AI-Native Automation System of the Future
28 August 2026
Integrating System Intelligence and Model Intelligence The next architecture of industrial automation: from L0–L3 hierarchical control to a dual-layer System-and-Model Intelligence framework. Industrial automation is entering a new era. For decades, automation has followed a clear, layered structure: L0: Sensors, drives, actuators, and instruments L1: Real-time control (PLC, AGC, AFC, sequence control) L2: Process models (rolling schedules, thermal models, setup calculations) L3: Production planning and plant management This L0–L3 architecture has served industry extremely well. It is reliable, deterministic, and highly engineered. And it will remain essential. But the next generation requires more: the ability to understand, reason, learn, and evolve—not just execute. The future is not simply “adding AI on top.” It is rethinking the architecture itself. Metals-Tech envisions a new AI-native industrial automation built on two complementary forms of intelligence: System Intelligence – The global brain Model Intelligence – The continuously evolving expert Together, they form a new control architecture that gradually transforms automation from predefined execution toward adaptive, predictive, and autonomous operation. System Intelligence: Understanding the plant as a whole Rather than focusing on one control loop or process model, System Intelligence continuously observes the complete production environment: Equipment condition Production schedule and material status Process stability and product quality Energy consumption, alarms, maintenance needs Operator actions and historical performance Traditional automation asks: “What should this controller do now?” System Intelligence asks: “What should the entire production system do next?” This is the transition from local control to global coordination, from alarm response to situation understanding, from operator-dependent decision making to AI-assisted industrial reasoning. Model Intelligence: Continuously evolving process knowledge Industrial production has always depended on models: Rolling force, forward slip, thermal, material deformation Flatness, crown, cooling, coiling, tension Furnace, mechanical property, energy, equipment degradation Traditionally, these models were static—built from physics, tuned during commissioning, and then fixed. AI changes this. The model can now continuously compare prediction vs. reality and improve itself. Physics First, AI Enhanced Pure black-box AI is not enough for industrial control. The most powerful architecture combines: Physical Model + Metallurgical Knowledge + Historical Data + Real-Time Data + Machine Learning + Adaptive Optimization AI doesn't replace physics. It enhances it.Physics provides structure. AI provides adaptation. From fixed models to self-evolving models Production never stops changing: raw materials, product mix, roll condition, equipment age, lubrication, ambient conditions, new products. A static model gradually becomes less representative. Model Intelligence turns the model into a living component of the automation system—continuously evaluating its own predictions, learning, and adapting. System Intelligence: Coordinating the whole plant Consider a hot rolling mill. A traditional system independently controls furnace, descaling, roughing, finishing, cooling, coiling, tracking. An AI-native system understands the relationships among them. Abnormal slab temperature → higher rolling force → gauge deviation → finishing temperature change → mechanical property shift → coiling adjustment → quality attention required. Traditional automation sees several signals. System Intelligence sees one production event. That distinction is fundamental. The AI-Native Control Loop Traditional control: Target → Execute → Measure → Correct AI-native automation adds a cognitive cycle: Observe → Understand → Predict → Optimize → Execute → Verify → Learn This creates a continuous loop of perception, reasoning, optimization, and learning. What happens to Level 0–Level 3? They remain. Deterministic automation must stay deterministic: emergency stops, protection logic, high-speed drive control, millisecond-level hydraulic control, safety interlocks. AI provides a higher level of perception, prediction, optimization, and coordination. The result is a hybrid architecture: Deterministic LayerIntelligent LayerSafety, real-time control, sequence execution, motion control, technological regulationUnderstanding, prediction, optimization, learning, reasoning, decision support Industrial reliability + intelligent adaptability. Digital Twin becomes the plant’s world model In AI-native automation, the Digital Twin becomes more than visualization—it becomes the contextual brain of the system: What equipment exists and how it is connected What material is being processed and where What process conditions exist What constraints and production targets apply The plant changes from a collection of data tags into an understandable industrial environment. Data becomes industrial memory Data alone is not intelligence. The AI-native plant transforms data into structured memory. Every coil, slab, and product can contribute to the plant's knowledge: Which setup produced the best quality? Which conditions preceded a defect? Which parameter combination created instability? Which strategy minimized energy? Data becomes Memory.Models become Knowledge.AI becomes Reasoning.Automation becomes Action. The human role will also change AI-native automation does not remove industrial experts. It changes how their expertise is used. The operator evolves from Machine Operator → Production Supervisor → Industrial Intelligence Supervisor. AI becomes an engineering partner—not a replacement, but an amplifier of human knowledge. From automation to autonomy The long-term journey toward the Autonomous Plant can be understood in five stages: Automated – Machines execute predefined logic Connected – Data becomes visible across systems Predictive – Models anticipate quality and process behavior Adaptive – The system optimizes in changing conditions Autonomous – The plant continuously optimizes with limited human intervention The critical transition is not Manual → Automatic.It is Automatic → Intelligent → Autonomous. Why metals production is a natural fit Metals manufacturing is: Continuous and dynamic Highly coupled and energy intensive Metallurgically complex and quality critical Small upstream deviations create large downstream consequences. This is precisely where System Intelligence and Model Intelligence create value. The Metals-Tech vision AI changes the technology, but process is still the core. The value of industrial AI will be measured by production results: better gauge, flatness, surface, mechanical properties; higher yield, throughput; lower energy, downtime; faster product development, more stable production. AI without process knowledge is only an algorithm.Process knowledge without learning remains static.The combination creates industrial intelligence. Conclusion: Beyond L0–L3 The L0–L3 architecture will remain the deterministic foundation. But the architecture of intelligence is changing. The next generation of automation will be defined by how the entire production system understands, predicts, optimizes, and learns. This is: System Intelligence + Model Intelligencebuilt upon L0–L3leading toward Autonomous Production. Not AI added to automation.Automation designed for AI from the beginning. Not isolated intelligent functions.A continuously learning production system. Not simply a smarter controller.A smarter plant. This is the future of AI-native industrial automation—and it is already beginning.
Read More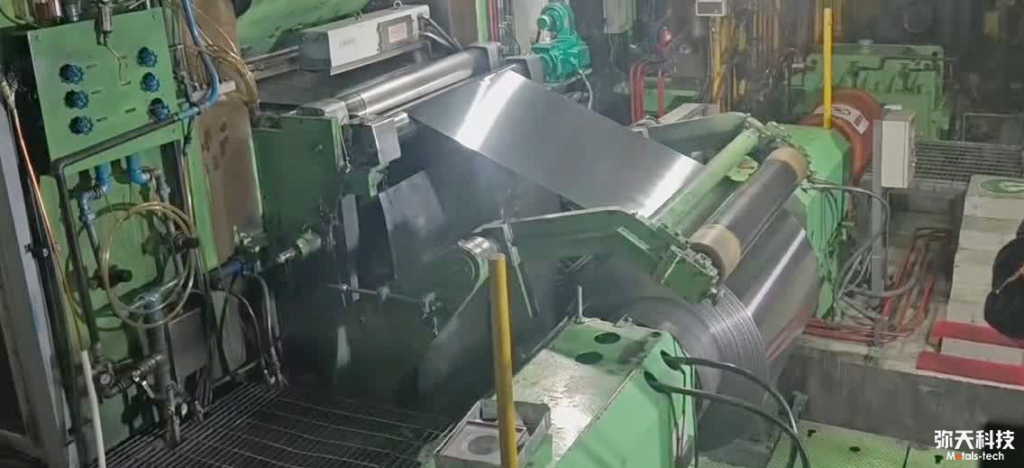
From 45°C Liquid Cooling to High-End Aluminium Materials
25 August 2026
Metals-Tech Enables the Material Foundation of Next-Generation AI Computing Infrastructure ▍The AI infrastructure shift is also a materials shift As large-scale AI models and GPU clusters expand rapidly, the performance bottleneck is shifting from chip supply to power delivery, thermal management, and advanced materials capability. NVIDIA's latest liquid-cooling architecture for AI infrastructure signals a clear industry trend: future AI data centers will be denser, run hotter, and depend increasingly on liquid cooling. Warm-water cooling at around 45°C enables AI factories to significantly reduce energy consumption and water usage while improving overall system efficiency. Behind this transformation lies a growing demand for high-end aluminium materials—from cold plates, heat exchangers, and dry coolers to fin stock, structural components, and laminated foil for power electronics. ▍High-end aluminium: the material backbone of AI cooling Warm-water liquid cooling relies on a complete material system that is lightweight, thermally efficient, and scalable: Heat exchanger materials – Fin stock, tubes, brazing sheets, and precision-formed components require excellent thickness accuracy, stable mechanical properties, high surface cleanliness, and reliable brazing performance. Cold plate and thermal management components – Aluminium is widely used in manifolds, covers, structural cooling parts, and auxiliary cold plates—demanding tight flatness, surface quality, corrosion resistance, and machining stability. Laminated foil for power electronics – AI computing also drives demand for intelligent power distribution. Solid-state transformers (SST) and power conversion systems rely on high-quality laminated foil—directly connecting aluminium foil rolling to AI infrastructure. ▍Metals-Tech: building quality into every step. High-end aluminium materials cannot be created by final inspection alone. Quality must be designed, controlled, and verified across the entire production process. Metals-Tech provides integrated Electrics, Automation, and Digital solutions across the full aluminium production chain: Hot rolling – Precision temperature control, rolling schedule optimization, gauge and profile management, and coiling control to establish a stable material foundation. Cold rolling – High-response AGC, automatic flatness control, mass flow control, tension optimization, laser speed measurement, edge plasticity improvement, and full-coil digital quality reporting. Foil rolling – Mass flow AGC, AFC, edge defect prevention, digital quality reporting, and adaptive process models to produce ultra-thin foil for high-end power electronics. All systems are integrated through our Metals Intelligence digital platform, enabling real-time quality traceability from melt to final coil. ▍From rolling control to AI infrastructure. The AI liquid-cooling revolution is creating a new demand structure for aluminium producers. Entering this market requires more than capacity—it demands stable quality, low defect rates, digital traceability, and the ability to continuously improve process performance. Metals-Tech helps aluminium producers meet these requirements through systematic control optimization and digital quality management—connecting rolling-mill performance directly to AI computing infrastructure. ▍Conclusion: NVIDIA's 45°C full liquid-cooling architecture points the way forward: higher density, higher efficiency, lower water use, and smarter thermal management. Aluminium will become one of the most scalable materials for AI data center infrastructure—from dry coolers and heat exchangers to fin stock, structural parts, and power-electronics systems. Metals-Tech helps aluminium producers manufacture these high-end materials through full-process automation, digital quality management, and advanced process control. From liquid cooling to electric power, from aluminium rolling to AI factories—Metals-Tech enables the material foundation of green, efficient, and intelligent computing infrastructure. Related Solutions: Aluminium hot rolling Aluminium cold rolling and foil rolling
Read More
Mass Flow Control Improves Aluminium Foil Rolling Quality
04 June 2026
Turning Ultra-Thin Foil Rolling into a Stable, Measurable and Repeatable Process Aluminium foil rolling is one of the most demanding processes in the non-ferrous metals industry. As strip thickness moves into the ultra-thin range, even a very small deviation in speed, tension, roll force, coolant condition or incoming material thickness can directly affect final product quality. For high-end foil products, quality is no longer judged only by final thickness. Producers must control the complete rolling condition of the coil: gauge accuracy, flatness, strip tension, rolling stability, surface condition, coil shape and length-based quality consistency. This requires more than conventional feedback control. It requires a process-control philosophy based on mass flow stability. Metals-Tech applies advanced Electrics, Automation and Digital technologies to aluminium foil mills, helping producers transform foil rolling from an experience-driven process into a data-driven, model-supported and repeatable production system. The Challenge of Ultra-Thin Aluminium Foil Rolling In aluminium foil rolling, the material is extremely sensitive to process disturbances. When the exit gauge is reduced to around 0.128 mm or lower, the mill must maintain stable strip flow through the roll gap while balancing several interacting variables: Key VariableInfluence on Product QualityEntry and exit gaugeDetermines dimensional accuracy and downstream usabilityRolling speedAffects thermal balance, lubrication and control responseEntry and exit tensionInfluences elongation, flatness and strip stabilityRoll forceAffects gauge reduction and rolling bite conditionWork roll bendingCorrects strip shape and flatness distributionAcceleration and deceleration lengthDetermines transition loss and off-gauge materialCoil length trackingProvides basis for quality classification and traceability In this environment, a single control loop is not enough. Thickness, speed, tension and roll gap must work together as one coordinated system. This is where mass flow control creates value. Mass Flow: The Core Logic Behind Stable Gauge Control The principle of mass flow control is simple but powerful: the amount of material entering the roll gap must match the amount of material leaving the roll gap, considering strip speed and thickness. In practical mill control, this means that entry thickness, exit thickness, entry speed, exit speed, forward slip and tension behavior are continuously monitored and coordinated. When the system detects a deviation in strip flow, it can adjust the roll gap, speed reference or tension reference before the deviation develops into visible thickness error. This gives the foil mill three major advantages: Faster response to incoming material variationThe system does not wait for exit gauge error to become large. It reacts based on the relationship between material flow and rolling condition. Reduced off-gauge lengthDuring acceleration, deceleration, pass transition and speed fluctuation, mass flow control helps reduce unstable material length. More stable full-coil qualityGauge deviation can be controlled not only at selected points, but along the entire coil length. Typical Result: 99.76% In-Gauge Length at Production Speed The performance data in Figure 1 shows a representative aluminium foil rolling pass with strong quality stability. Coil and Product Information ItemValueEntry gauge0.152 mmExit gauge0.128 mmExit width1045 mmTotal coil length20,677 mSteady-state length20,586 mAverage rolling speedApprox. 309–313 m/minPass run time68 min 52 sec The pass achieved stable rolling over more than 20 km of strip length, which is a meaningful indicator for foil production. Long-coil stability is essential because even a small percentage of quality loss can become a large amount of downgraded material when the coil length is high. AGC Performance: Precise Thickness Control Across the Coil Automatic Gauge Control is one of the key functions for aluminium foil rolling. In the reported pass, the AGC result demonstrates excellent dimensional performance. AGC IndicatorResultContract sigma0.80%2 Sigma result0.22%3 Sigma result0.44%Off-gauge length above 150 m/min49.50 mPercent in gauge above 150 m/min99.76%ResultPassed This result shows that the actual gauge deviation was far better than the contract requirement. More importantly, the off-gauge length was limited to only 49.50 m during production-speed rolling. For aluminium foil producers, this directly improves yield, reduces trimming and downgrade loss, and supports stable delivery to high-end customers. AFC Performance: Flatness Stability for Downstream Processing For foil products, flatness is as important as gauge accuracy. Poor flatness can cause wrinkling, winding defects, unstable downstream slitting and reduced final product usability. The AFC performance in the same pass shows a stable flatness result: AFC IndicatorResultContract sigma6 I-units2 Sigma result1.27 I-units3 Sigma result3.37 I-unitsResultPassed The flatness profile remained stable over the steady-state rolling length. This indicates that work roll bending, tension control and shape feedback were well coordinated during the pass. For high-end foil products used in packaging, battery materials, electronic materials and precision industrial applications, such flatness stability is critical for downstream reliability. From Control Accuracy to Product Quality Mass flow control does not work alone. It is part of a complete control architecture that links field instruments, drive systems, Level 1 automation, technological control and Level 2 process models. Metals-Tech’s Aluminium Foil Rolling Control Architecture Incoming Material Data ↓Level 2 Setup Model ↓Speed / Tension / Roll Gap Preset ↓Mass Flow Control + AGC + AFC ↓Real-Time Feedback from Gauge, Flatness and Tension Systems ↓Adaptive Correction During Rolling ↓Full-Coil Quality Report and Traceability This architecture allows the mill to move from “after-the-fact quality inspection” to “in-process quality creation.” Instead of identifying defects only after rolling, the system continuously stabilizes the rolling process and records key quality indicators along the full coil length. Digital Reporting: Making Quality Visible A high-performance automation system must not only control the mill. It must also make production quality visible, measurable and traceable. The quality report shown in Figure 1 provides a complete view of the pass, including: Report AreaPurposeCoil time and pass durationTracks production efficiencyEntry and exit gaugeConfirms reduction targetSpeed, tension and roll forceShows rolling stabilityAGC performanceVerifies thickness accuracyAFC performanceVerifies flatness qualityLength distributionSeparates acceleration, steady-state and deceleration zonesTrend curvesSupports visual diagnosis and process optimization This type of reporting is especially valuable for aluminium foil producers serving demanding customers. It provides objective evidence of process capability and helps production teams identify opportunities for continuous improvement. Reducing Transition Loss in Acceleration and Deceleration In foil rolling, a large portion of off-gauge material often occurs during acceleration and deceleration. When speed changes, the relationship between roll gap, strip tension, forward slip and material flow also changes. If these variables are not coordinated, the mill may generate excessive transition scrap. In the reported case, acceleration and deceleration lengths were both controlled at approximately 46 m, while the steady-state length reached 20,586 m. This means the majority of the coil was produced under stable rolling conditions. For producers, this has direct economic value: Improvement AreaProduction BenefitShorter transition lengthLess off-gauge materialStable speed rampBetter gauge consistencyCoordinated tension controlLower risk of strip breakageReliable steady-state rollingHigher yield and productivityFull-coil data recordFaster quality analysis Metals-Tech’s Value for Aluminium Foil Producers Metals-Tech provides integrated Electrics, Automation and Digital solutions for aluminium cold rolling and foil rolling mills. Our technologies help customers improve rolling stability, product quality and production efficiency through a combination of real-time control and process intelligence. Key capabilities include: High-response Automatic Gauge ControlPrecise roll gap and speed coordination to maintain tight thickness tolerance during production rolling. Mass Flow ControlMaterial-flow-based control strategy to improve gauge stability, especially during speed change and thin-gauge rolling. Automatic Flatness ControlIntegration of flatness measurement, bending control and tension optimization to achieve stable strip shape. Advanced Drive and Tension ControlCoordinated main drive and reel control to maintain stable strip movement and reduce rolling disturbance. Level 2 Setup and Adaptive ModelsProduct-specific pass schedule, preset calculation and process learning to shorten commissioning and improve repeatability. Digital Quality ReportingFull-coil process data, AGC/AFC performance evaluation and traceable quality records for production, maintenance and customer audit. From Stable Rolling to Premium Foil Products The market for aluminium foil is moving toward thinner gauges, higher surface quality, stricter tolerance and more demanding downstream applications. Battery foil, electronic foil, high-barrier packaging foil and precision industrial foil all require stable process control and repeatable quality. Mass flow control provides a practical and powerful method for improving foil rolling performance. By coordinating speed, tension, roll gap and gauge feedback, it helps the mill maintain material continuity through the roll bite and reduce quality fluctuation over the full coil length. Metals-Tech combines this control philosophy with advanced automation, process models and digital reporting systems. The result is a foil rolling solution that supports higher yield, better quality consistency and stronger production confidence. Conclusion: Quality Is Created During Rolling In aluminium foil production, quality cannot be corrected at the end of the process. It must be created during rolling, meter by meter and coil by coil. The performance shown in this case demonstrates what intelligent control can deliver: stable rolling speed, precise gauge control, excellent flatness performance, low off-gauge length and full-coil traceability. With mass flow control as a core function, Metals-Tech helps aluminium foil producers build a more stable, more intelligent and more profitable rolling process. For the next generation of high-end aluminium foil products, the future belongs to producers who can control not only the mill, but the quality flow of the material itself.
Read More
Improving Edge Plasticity: From Edge Spraying to Induction Heating
04 June 2026
Metals-Tech’s Intelligent Approach to Edge Crack Control in High-Value Rolling In modern rolling production, product quality is no longer defined only by gauge accuracy and flatness. For high-value strip materials, especially aluminium alloys, stainless steel and advanced special alloys, edge quality has become one of the decisive factors affecting yield, downstream processing and final customer acceptance. Edge cracking, edge hardening, poor edge elongation and strip breakage are often caused by insufficient edge plasticity during rolling. These problems may appear first as small edge defects, but they can quickly develop into serious production losses: trimming increase, coil downgrade, unstable rolling, strip breakage and reduced delivery reliability. Metals-Tech focuses on the complete rolling process, combining metallurgical understanding with advanced Electrics, Automation and Digital solutions. Through intelligent edge control technologies, from edge spraying to induction heating, Metals-Tech helps producers improve edge plasticity, stabilize rolling and increase the value of finished products. Why Edge Plasticity Matters During rolling, the strip edge experiences a different deformation condition from the strip center. The edge area is more sensitive to temperature loss, stress concentration, uneven lubrication, work roll deformation and local metallurgical variation. When the edge becomes colder, harder or less ductile than the center area, it loses the ability to deform smoothly. As a result, micro-cracks can initiate at the edge and propagate along the rolling direction. In severe cases, the strip may break, leading to production interruption and equipment risk. For aluminium rolling, edge plasticity is especially important in high-strength alloys, wide strip production and thin-gauge rolling. For stainless steel and other hard materials, edge cracking can be even more difficult to control because rolling force, work hardening and thermal sensitivity are more complex. The key question is therefore clear: how can the rolling mill create a more uniform and more controllable deformation condition across the strip width? Typical Edge Quality Problems in Rolling ProblemMain CauseProduction ImpactEdge crackingLow edge temperature, excessive edge hardening, stress concentrationCoil downgrade, trimming loss, strip break riskEdge wavinessUneven transverse deformation and thermal distributionPoor flatness, unstable downstream processingEdge overcoolingExcessive coolant or poor spray distribution near strip edgeReduced plasticity and increased crack sensitivityEdge surface defectUnstable lubrication, coolant carry-over or local roll contact issueSurface rejection and customer complaintPoor trimming yieldWide defect zone near edgeLower metal yield and higher production cost Edge plasticity control is therefore not only a quality function. It is a yield function, a safety function and a productivity function. From Edge Spraying to Induction Heating: A Technology Evolution For many rolling mills, the first step of edge control starts with edge spraying. By controlling coolant or lubricant distribution near the strip edge, the mill can reduce local overcooling, improve lubrication condition and stabilize the roll bite. However, as product requirements become more demanding, passive or semi-active control methods may not be enough. High-strength aluminium alloys, battery materials, automotive sheet, stainless steel strip and ultra-thin products require a more precise approach to edge thermal management. This is where edge induction heating becomes a powerful technology. Instead of only reducing cooling intensity, induction heating actively supplies energy to the edge zone. It improves local temperature, increases ductility and reduces the tendency of edge cracking during rolling. Conventional Rolling ↓Edge overcooling / uneven deformation ↓Edge hardening and crack initiation ↓Trimming loss, downgrade or strip breakIntelligent Edge Plasticity Control ↓Edge spraying + edge thermal model + induction heating ↓Controlled edge temperature and deformation condition ↓Reduced edge cracking, higher yield and stable rolling Edge Spraying: The First Layer of Edge Quality Control Edge spraying is an effective and practical method for improving edge stability. It allows the automation system to adjust coolant or emulsion distribution according to strip width, rolling speed, alloy grade, pass schedule and edge condition. In a conventional system, coolant is often applied across the full strip width with limited local flexibility. This may create excessive cooling at the edge area, especially when strip width changes or spray alignment is not optimized. Metals-Tech’s edge spraying control can be integrated with mill automation to provide: Strip-width-based spray zone control Edge masking and edge cooling reduction Recipe-based coolant distribution Speed-related spray compensation Pass-based edge cooling optimization Data recording for quality analysis The target is not simply to use less coolant. The target is to create a better deformation environment at the edge, while maintaining stable rolling temperature, lubrication and surface condition. Induction Heating: Active Edge Thermal Compensation While edge spraying can reduce unwanted cooling, induction heating can actively improve edge plasticity by adding heat to the edge area before or during rolling. Induction heating has several important advantages for edge quality control: AdvantageValue for Rolling ProductionLocalized heatingEnergy is focused on the edge zone without heating the full strip widthFast responseHeating power can be adjusted quickly according to process conditionClean processNo flame, no contact and no additional surface contaminationPrecise controlSuitable for automation, recipes and closed-loop temperature controlHigh flexibilityCan be applied to different alloys, widths and production strategies By increasing the temperature of the edge zone, induction heating improves local ductility and reduces the risk of crack initiation. It is especially valuable when rolling materials with narrow process windows, high alloy content or strong work-hardening behavior. Metals-Tech’s Integrated Control Philosophy Metals-Tech does not treat edge spraying or induction heating as isolated devices. They are part of a complete process-control architecture connecting Level 0 instruments, Level 1 automation, Level 2 models and digital quality systems. The system can coordinate edge control with rolling speed, reduction schedule, strip tension, coolant system, roll bending, flatness control and quality tracking. Product Recipe / Alloy Grade / Strip Width ↓Level 2 Process Setup ↓Edge Plasticity Strategy Selection ↓Edge Spraying Control + Induction Heating Preset ↓Real-Time Signals:Temperature / Speed / Tension / Rolling Force / Flatness / Edge Defect Feedback ↓Level 1 Closed-Loop Adjustment ↓Coil Quality Report and Process Learning This architecture enables the mill to apply the right strategy for the right product. Some products may need only optimized edge spraying. Others may require induction heating during critical passes. For premium products, both methods can be combined into a coordinated edge plasticity control system. Application Scenarios Edge plasticity improvement is especially valuable in the following applications: ApplicationMain RequirementEdge Control BenefitAutomotive aluminium sheetSurface quality, forming performance, stable trimmingReduced edge crack and improved delivery qualityBattery aluminium materialsThin gauge, high cleanliness, stable strip travelLower breakage risk and higher yieldHigh-strength aluminium alloysNarrow rolling window and crack sensitivityImproved deformability and process stabilityStainless steel stripHigh rolling force and work hardeningReduced edge splitting and trimming lossPrecision foil and thin stripStable tension and full-coil consistencyFewer edge defects and better downstream slitting For producers, the benefit is not limited to one process step. Better edge plasticity improves the entire production chain: rolling, annealing, trimming, slitting, coating, forming and final customer use. Digital Quality: Making Edge Performance Visible Edge problems are often difficult to solve because they are affected by many variables at the same time. A crack may appear at the end of rolling, but its cause may come from earlier temperature loss, coolant instability, tension disturbance or incoming material variation. Metals-Tech’s digital quality platform helps production teams connect edge defects with process history. Key data can be collected and analyzed coil by coil, meter by meter: Data CategoryTypical SignalsRolling conditionSpeed, force, torque, roll gap, reductionThermal conditionEntry temperature, edge temperature, cooling intensity, induction powerStrip conditionGauge, width, tension, flatness, edge positionActuator statusSpray valve status, heater power, bending force, coolant pressureQuality resultEdge crack record, trimming width, surface inspection, downgrade reason With this data foundation, the mill can move from manual troubleshooting to model-based optimization. Operators can identify which products are sensitive to edge cracking, which passes require additional heating, and which coolant strategies deliver the best result. From Process Stability to Economic Value Improving edge plasticity creates direct and measurable production value. ImprovementBusiness ValueReduced edge cracksHigher prime yield and fewer downgraded coilsLower trimming widthMore saleable metal from each coilFewer strip breaksHigher mill availability and safer operationStable downstream processingBetter slitting, coating, forming and customer performanceRepeatable recipesFaster product development and shorter learning curveDigital traceabilityStronger customer confidence and audit support For high-value materials, even a small improvement in edge yield can generate significant annual economic benefit. When combined with reduced stoppage time and improved delivery reliability, edge plasticity control becomes a strategic technology rather than a local quality function. Metals-Tech’s Role: A Partner for Intelligent Rolling Metals-Tech provides full-stack Electrics, Automation and Digital solutions for the metals industry. Our capabilities cover field instruments, drive systems, Level 1 automation, Level 2 process control, digitalization, commissioning, performance optimization and lifecycle service. In edge plasticity improvement, Metals-Tech can support customers through: Process DiagnosisAnalyzing existing edge defects, rolling data, product mix and equipment configuration. Automation IntegrationConnecting edge spraying, induction heating, temperature measurement and mill control into one coordinated system. Model-Based SetupCreating product-specific recipes for edge cooling, edge heating and rolling strategy. Closed-Loop ControlUsing real-time process signals to adjust edge control parameters during production. Digital ReportingBuilding coil-based quality reports and long-term performance analysis for continuous improvement. Lifecycle OptimizationSupporting tuning, upgrades and product expansion after commissioning. Conclusion: Edge Quality Starts with Edge Plasticity In high-value rolling, the strip edge is often the weakest point of the process. But with the right technology, it can also become one of the strongest indicators of mill intelligence. From edge spraying to induction heating, edge plasticity control represents a clear direction for modern rolling mills: more precise thermal management, more coordinated automation and more data-driven quality improvement. Metals-Tech helps producers turn this direction into practical performance. By integrating edge control into the full rolling automation and digital quality system, we enable customers to reduce edge cracks, improve yield, stabilize production and deliver higher-value materials to demanding markets. In the future of rolling, quality will not be created only at the strip center. It will be created across the full width — from centerline to edge, from the first meter to the last meter, from process data to customer value.
Read More
Eliminating “Slip” Error in High-Precision Control: Laser Speed Measurement for Cold Rolling Mills
04 June 2026
From roll-based estimation to true strip speed measurement In high-precision cold rolling, speed is not only a production parameter. It is one of the fundamental signals behind gauge control, tension control, elongation control, mass flow calculation and coil quality evaluation. Traditionally, strip speed is often calculated from motor encoder feedback, roll diameter, bridle roll speed or reel speed. These methods are practical and widely used, but they share one unavoidable limitation: they do not always represent the true strip speed. Between the strip and the deflector roll (measuring roll), there may be slip. Between the work roll and the strip, there may be slip. During acceleration, deceleration, tension fluctuation, roll wear, lubrication change or thin-gauge rolling, these slip effects become more significant. For conventional production, the error may be acceptable. For high-end cold rolling, foil rolling, battery materials, automotive sheet and precision stainless steel, the same error can become a direct source of quality deviation. Metals-Tech applies laser speed measurement technology to cold rolling mills, integrating non-contact true speed feedback into Level 1 automation, AGC, AFC, tension control, elongation control and Level 2 process models. The result is a more accurate, more stable and more intelligent rolling process. Why Slip Error Matters Cold rolling is a process of controlled deformation. The strip is reduced, elongated and tensioned as it passes through the mill. To control this process precisely, the automation system must know how fast the material is actually moving. However, when speed is inferred from rotating components, the measurement may contain hidden errors. Encoder speed ↓Roll diameter compensation ↓Calculated strip speed ↓Possible error sources:roll wear / roll thermal expansion / No-load loss of rolls varies with seasons and ambient conditions /strip-roll slip / tension change / surface condition The problem is not that encoder feedback is unreliable. The problem is that encoder feedback measures the rotation of a mechanical part, not the movement of the strip itself. For a high-speed cold rolling mill, even a small speed error can influence: Control FunctionImpact of Slip ErrorMass flow AGCIncorrect entry/exit flow calculation and gauge deviationTension controlUnstable tension reference and compensation errorElongation controlIncorrect elongation calculation in skin pass or tension levelerCoil length calculationInaccurate production length and yield recordSpeed synchronizationThe entry and exit deflector rolls/bridle rolls and reels are precisely synchronized with strip speed to prevent scratch damage on the strip surface.Product quality analysisDistorted process data and root-cause diagnosis In high-end production, the control system must eliminate uncertainty at the signal source. Laser speed measurement provides this foundation. Laser Speed Measurement: Measuring the Strip, Not the Roll Laser speed measurement is a non-contact technology that directly measures the moving strip surface. It does not rely on roll diameter, roll contact, mechanical friction or encoder conversion. Therefore, it can provide true strip speed even when slip occurs between the strip and the roll. The measurement principle is simple in concept but powerful in application: the sensor detects the movement of the strip surface and outputs a high-precision speed signal to the automation system. This signal can then be used as the reliable reference for advanced control functions. Key advantages FeatureValue for Cold RollingNon-contact measurementNo mechanical wear, no roll contact errorTrue strip speedEliminates slip between strip and deflector roll (measuring roll)Fast responseSuitable for dynamic control during acceleration and decelerationHigh repeatabilityImproves process stability and quality consistencyDigital integrationCan be connected to PLC, drive system, AGC and Level 2 modelsBetter traceabilityProvides accurate speed and length records for each coil From Speed Accuracy to Gauge Accuracy Automatic Gauge Control relies heavily on accurate process feedback. In many cold rolling mills, mass flow control is one of the most effective methods for improving thickness accuracy. It compares the material flow entering and leaving the roll gap: Entry thickness × Entry speed ≈ Exit thickness × Exit speed If entry or exit speed is calculated with slip error, the mass flow calculation is no longer fully reliable. The control system may compensate for a deviation that does not truly exist, or miss a deviation that has already started to develop. With laser speed measurement, the mass flow calculation becomes more accurate because the system uses true strip speed rather than roll-derived speed. Laser entry speed + laser exit speed ↓More accurate mass flow calculation ↓Faster AGC response ↓Lower off-gauge length ↓Higher full-coil thickness consistency For thin-gauge aluminium/copper, battery materials and high-precision stainless steel, this improvement can directly reduce off-gauge length, improve yield and support stricter product tolerance. Improving Tension and Elongation Control In cold rolling and skin pass rolling, tension and elongation are closely related to strip speed. When the system uses roll-based speed estimation, slip can lead to inaccurate elongation calculation. This is especially important in: Skin pass mills Tension levelers Recoiling lines Aluminium foil mills Battery foil production lines High-strength steel and stainless steel lines For example, in skin pass rolling, the required elongation may be very small but must be controlled very precisely. A small speed measurement error between entry and exit sides may result in incorrect elongation feedback. Laser speed measurement helps eliminate this error and improves the reliability of elongation control. ApplicationBenefit of Laser Speed MeasurementSkin pass millMore accurate elongation controlTension levelerBetter extension and flatness stabilityCold rolling millImproved mass flow and gauge controlFoil millReduced speed-related gauge fluctuationProcessing lineMore accurate length, speed and coil trackingBattery material lineHigher stability for thin and sensitive products Reducing Transition Loss During Acceleration and Deceleration Rolling speed is not constant during the entire coil. At the head and tail of the strip, the mill must accelerate and decelerate. These transition zones are often the most difficult areas for gauge and tension control. During speed change, slip conditions may also change. Lubrication, roll bite condition, strip tension and forward slip are all dynamic. If the control system depends only on mechanical speed feedback, it may not fully capture the actual strip behavior. Laser speed measurement provides real-time true speed during these dynamic phases. This allows the control system to improve: Process PhaseControl ImprovementThreadingMore reliable strip movement detectionAccelerationBetter speed synchronization and mass flow correctionSteady rollingStable reference for AGC and tension controlDecelerationReduced tail-end off-gauge lengthTail-outMore accurate length and coil-end tracking Metals-Tech’s Integrated Automation Architecture Metals-Tech does not treat laser speed measurement as an isolated instrument. It is integrated into the full automation and digital control architecture of the rolling mill. Laser Speed Sensor ↓Signal Processing Unit ↓Level 1 PLC / APC System ↓AGC / Tension / Elongation / Mass Flow Control ↓Drive System and Actuator Coordination ↓Level 2 Model and Coil Quality Report ↓Data Analysis and Process Optimization This integration enables the sensor value to become a real control variable, not only a display signal. The measured true speed can be used for: Entry and exit strip speed feedback Mass flow AGC calculation Forward slip setup and monitoring Tension control compensation Elongation control Speed synchronization Coil length calculation Quality report generation Model adaptation and process learning Through this architecture, laser speed measurement becomes part of the mill’s intelligent control system. Detecting and Understanding Slip One additional advantage of laser speed measurement is that it makes slip visible. When the system has both encoder-based roll speed and laser-based strip speed, it can calculate the actual difference between them. This provides valuable process information. Roll surface speed – True strip speed = Slip-related deviation By monitoring this deviation, operators and engineers can better understand the rolling process. Slip trends may indicate changes in lubrication, roll surface condition, tension balance, strip surface quality or rolling force. Slip TrendPossible Process MeaningIncreasing roll-strip deviationLubrication change or unstable roll biteSudden speed mismatchTension disturbance or strip movement abnormalityPass-dependent slip patternProduct-specific deformation behaviorWidth or alloy-related variationDifferent surface and plasticity conditionsAbnormal tail-end slipDeceleration or winding instability This transforms slip from a hidden error into a measurable process indicator. Digital Quality: Accurate Speed Data for Full-Coil Traceability For premium cold-rolled products, customers increasingly require not only final quality results but also process evidence. Accurate speed data is an important part of this evidence. With laser speed measurement, Metals-Tech’s digital quality system can record true strip speed, length, acceleration, deceleration, mass flow deviation and speed synchronization status for each coil. The system can connect speed data with: Data CategoryTypical SignalsThickness qualityEntry gauge, exit gauge, AGC deviation, off-gauge lengthShape qualityFlatness signal, bending force, tilting, zone coolingTension conditionEntry tension, exit tension, reel torque, bridle statusSpeed conditionLaser speed, encoder speed, acceleration, slip deviationProcess conditionRolling force, motor current, coolant status, pass scheduleCoil recordLength, product grade, customer requirement, quality judgment This provides a stronger basis for process optimization, customer audit and continuous improvement. Practical Benefits for Producers Laser speed measurement creates value by improving both control accuracy and process transparency. Improvement AreaProduction ValueElimination of slip errorMore reliable control inputBetter AGC performanceLower thickness deviation and off-gauge lengthMore accurate elongation controlHigher quality in skin pass and tension levelingImproved speed synchronizationReduced strip instability and transition loss, eliminate surface scratches on the stripAccurate coil lengthBetter yield calculation and production reportingSlip monitoringBetter diagnosis of lubrication and roll bite conditionsDigital traceabilityStronger process evidence for premium customers For producers of aluminium/copper cold strip, foil, battery foil, automotive sheet, stainless steel and precision strip, these improvements are directly connected to product quality and commercial value. Application Fields Laser speed measurement is especially suitable for production lines where high precision and high repeatability are required. FieldTypical Product RequirementAluminium/Copper cold rollingTight gauge tolerance and stable mass flowAluminium/Copper foil rollingUltra-thin gauge and high-speed stabilityBattery foilHigh consistency, low defect rate and precise lengthAutomotive sheetStable process data and premium surface qualityStainless steel rollingAccurate tension and speed under high rolling forceSkin pass rollingPrecise elongation and surface finishingTension levelingAccurate extension and flatness correctionProcessing linesReliable speed, length and tracking control Metals-Tech's Role: From Instrument Signal to Intelligent Control A sensor alone does not create performance. The value comes from how the signal is integrated, filtered, validated and used by the automation system. Metals-Tech provides complete engineering support for laser speed measurement applications, including: Process AnalysisIdentifying where slip error affects quality, yield or control stability. Sensor Selection and LayoutDefining the best measuring position, installation angle, protection method and signal interface. Level 1 IntegrationConnecting laser speed feedback with PLC, APC, drive system and technological control. Control Function UpgradeUsing true speed feedback in AGC, tension control, elongation control and mass flow control. Level 2 and Digital ConnectionApplying speed data to setup models, coil tracking, quality reports and long-term process analysis. Commissioning and OptimizationTuning control parameters, validating measurement accuracy and improving production performance. Conclusion: True Speed Creates True Control In high-precision cold rolling, hidden speed error can become hidden quality loss. Slip between the strip and mechanical measuring rolls may be small, but its influence on gauge control, tension control, elongation control and quality traceability can be significant. Laser speed measurement provides a direct and effective solution. By measuring the true movement of the strip, it eliminates slip-related error at the source and gives the automation system a more reliable foundation for control. Metals-Tech integrates laser speed measurement into the full cold rolling control architecture, turning true strip speed into better AGC performance, more accurate elongation control, improved precise speed matching, improved transition stability and stronger digital quality evidence. For the next generation of precision rolling, control accuracy begins with measurement accuracy. And measurement accuracy begins with seeing the strip itself.
Read More